

การลบคมแผ่นโลหะที่ตัดด้วยเลเซอร์: วิธีเลือกวิธีการและเครื่องจักรที่เหมาะสม
ต.ค. 30 ,2026
How to Choose the Right Method and Machine
Short answer: Laser-cut parts almost always need a finishing pass. Small parts in volume usually go through a vibratory tumbler. Flat parts and panels go through a brush or wide-belt เครื่องขัดแต่งเสี้ยน. Parts with tight tolerances and complex contours can justify laser deburring. If you’re running production, an automated machine pays for itself in consistency and labor.
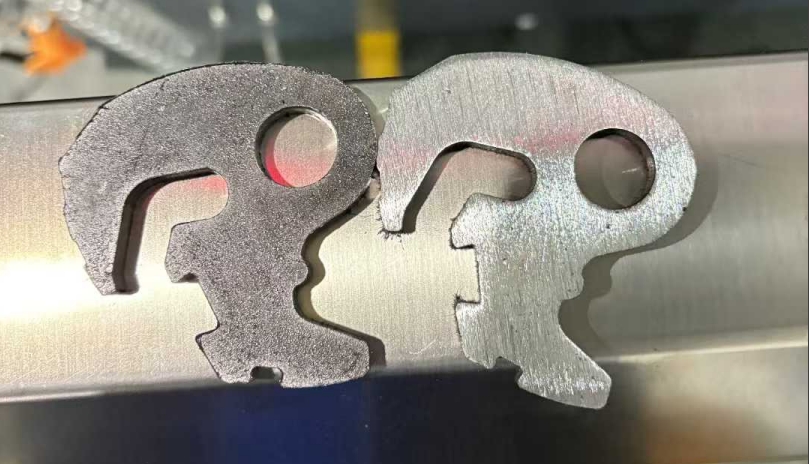
Why a clean laser cut still isn’t finished
A laser leaves a tidy-looking edge, but “tidy-looking” isn’t the same as “ready.” Depending on your cutting gas, speed, material and thickness, you can end up with:
- หนาม: small raised lips of metal along the cut
- Slag and dross: molten metal that re-solidified on the underside
- Oxide: a hard, dark layer, common when oxygen is the assist gas
- Razor edges: even a perfect cut is sharp enough to slice a glove
Each one causes a different headache. Sharp edges hurt people and chew through cables. Slag and oxide ruin coating adhesion. Burrs throw off fit-up and weld seams. None of it is cosmetic.
Know your burr before you buy a machine
Machines get bought to solve a specific defect, so identify yours first.
| Defect | What causes it | What it ruins |
|---|---|---|
| Breakout burr | Material shears unevenly during the cut | Handling safety, coating grip |
| Rollover or tear burr | Material deforms or tears at the edge | Fit and surface consistency |
| Slag / spatter | Molten metal freezing on the edge or underside | Finish quality, coating |
| Oxide layer | Oxidizing assist gas | Coating adhesion, welding |
| Sharp corners | Just the nature of a cut edge | Safety, paint coverage |
If your shop sees mostly light burrs, you need something very different from a shop fighting heavy slag.
The main deburring methods, compared
Manual (files, grinders, abrasive wheels). Fine for prototypes and one-offs, and the only option for awkward spots. The trouble starts at volume: it’s slow, results vary from person to person, and hands get hurt.
Vibratory or tumble finishing. Parts and abrasive media vibrate together in a tub. It handles lots of small and medium parts at once, reaches holes and internal edges, and keeps the cost per part low. It’s a poor fit for big flat panels, and you get less control over the edge shape.
Wide-belt machines. Flat parts pass under an abrasive belt that knocks off burrs and works the edges. This is a workhorse for sheet and plate.
Rotary brush machines. Wire, nylon or abrasive brushes sweep the edges and surfaces. They remove burrs, round edges, and clean off oxide and slag residue. Good for sheet metal in general.
Laser deburring. A focused beam melts or vaporizes the burr and can reflow the edge into a smooth profile. You get precision and very little mechanical stress, which suits complex or tight-tolerance parts. The downsides are cost, a specialized setup, lower throughput than mass finishing, and trouble with heavy slag.
Combined lines. Many shops chain several steps, such as brush edge rounding, then belt surface finishing, then tumbling. One pass through a multi-station machine can deburr, round, remove oxide and finish the surface.
Matching the method to your parts
- Small parts, high volume: vibratory or tumble finishing
- Flat sheet and large panels: wide-belt or brush machines
- Lots of slots and holes: vibratory, brush, or laser deburring
- Steel and stainless: brush or belt both work well
- Aluminum and soft metals: use gentler abrasives and a controlled process, since thin or soft sheet is easy to over-grind or distort
- Tight tolerances, minimal distortion: laser deburring
- Prototypes and small batches: manual or vibratory
- Medium to large production runs: an automated deburring line
Edge rounding is its own requirement
Deburring takes material off. Edge rounding shapes the edge to a defined radius. They overlap, but they’re not the same job.
Rounding matters most when parts are going to be coated. Paint and powder pull away from sharp corners and leave them thin, which is exactly where corrosion starts. A rounded edge holds an even film. R2 is a widely used benchmark in Europe for safety and powder-coat adhesion, though the right radius depends on your industry and the part’s job. If a customer spec calls for one, confirm your machine can hit it repeatably.
A practical workflow
- Laser cut the parts.
- Inspect for burrs, slag and oxide.
- Deburr and round the edges with the method that fits the part.
- Finish the surface if needed (oxide removal, smoothing for coat or weld).
- Inspect again for burr-free edges, finish and dimensions.
- Coat, weld or assemble.
Skipping the second inspection is the mistake that costs the most. Leftover slag or oxide usually shows up as a coating failure or a bad weld, long after the part left your floor.
Why production shops move to automated machines
- ความสามารถในการทำซ้ำ: the ten-thousandth part has the same edge as the first.
- Labor: one operator and a machine replace several people at grinders.
- ความปลอดภัย: less hand contact with sharp parts, dust and swarf.
- Flexibility: modern machines combine brushes, abrasive belts, vacuum and magnetic work holding, so one machine covers many part types.
- Finish quality: you ship parts that are burr-free, edge-rounded and ready for coating, not just “good enough.”
Mistakes worth avoiding
- Relying on hand deburring for production volumes
- Using abrasives or a machine that’s wrong for the material, especially on aluminum and thin sheet
- Skipping inspection after deburring
- Ignoring edge roughness before welding or coating
What to ask before you buy
Have these answers ready before you talk to any machine supplier:
- What material and thickness range do you cut?
- Is the problem light burrs, heavy slag, or oxide?
- What’s your largest and smallest part?
- How many parts per shift?
- Do you need a specific edge radius?
- What happens next: powder coat, paint, weld or assembly?
A supplier who can’t get specific once you hand over those answers isn’t the right one. Ask to run your own sample parts before you commit.
คำถามที่พบบ่อย
Why do laser-cut parts need deburring?
Laser cutting can leave micro-burrs, oxide and sharp edges. Removing them makes parts safer to handle, helps coatings stick, and keeps assembly fits accurate.
What’s the difference between deburring and edge rounding?
Deburring removes unwanted material. Edge rounding shapes the edge to a set radius, which improves safety and coating adhesion.
Can manual deburring replace a machine?
For very small batches, yes. For production volumes it’s slow and inconsistent, and it depends heavily on who’s doing it.
What’s the best method for laser-cut stainless steel?
Rotary brushes or wide-belt grinding, depending on thickness and the finish you need.
How do I remove heavy slag from plasma-cut parts?
Heavy slag needs aggressive mechanical removal first, typically a slag hammer or a high-pressure drum system, followed by secondary finishing.
Why does oxide need to be removed?
Oxide forms when oxygen is the cutting gas. It leaves a hard, brittle edge layer that interferes with coating, welding and surface finishing.
Does edge rounding help powder coating?
Yes. Rounded edges let the coating spread evenly, which improves corrosion resistance and reduces thin spots on corners.
Can one machine handle burrs, slag and finishing?
Multi-station machines with drum heads, brushes and abrasive belts can cover several of these in a single pass.